

Die-Cut Design Rules
These are the steel rule die design limits Mag-Knight applies to every drawing, and the same rules the Mag-Knight Instant Pricing estimator checks automatically. Parts that break a rule can usually still be made, but they may cost more or need a design change. All values are in inches.
| Design rule | Limit | Why it matters |
|---|---|---|
| Minimum spacing between parallel cut lines | At least 1× material thickness | Applies to cut-to-cut and hole-to-hole web. Rule closer than the material thickness can crush, tear or distort the material, and slugs can pack into the die. |
| Hole-to-edge web, holes up to 5/8″ (0.625″) dia. | At least 1× hole diameter | Example: a 0.25″ hole needs at least 0.25″ of material to the part edge. |
| Hole-to-edge web, holes over 5/8″ dia. | At least 0.30″ | A thinner web can tear, stretch or pull out during cutting. |
| Minimum inside bend radius, soft materials (thin rule) | 1/16″ (0.0625″) | Sharper inside corners are rounded to the rule’s minimum radius. |
| Minimum inside bend radius, hard materials (thick rule) | 3/32″ (0.094″) | Hard plastics and higher-durometer rubber need thicker rule. |
| Holes and cutouts under 0.25″ | Allowed, priced as a complex part | Holes under 0.125″ also slow the press. |
| Slots, notches and tabs narrower than 0.25″ | Allowed, priced as a complex part | |
| Non-round cutouts under 0.5″ (smallest side) | Allowed, priced as a complex part | |
| More than 10 cutouts in one part | Allowed, priced as a complex part | |
| Parts smaller than 1″ × 1″ | Allowed, priced as a complex part | |
| Maximum foam thickness | 1″ closed-cell / 2″ open-cell | Foam over 1/2″ needs taller rule, which adds about 25% to the die. |
| Maximum press area per hit | 30″ × 60″, about 500″ of rule | Up to 7 cavities per die. |
| Key-feature tolerance | ±0.005″ | When called out on the drawing and verified with SPC. |
| General tolerance | ±0.015″ | |
| Unspecified tolerance | ±0.032″ | |
| Minimum order | 5 pieces | No setup fees. |
Watch the design-rule videos for examples of holes too close to an edge, cuts too close together, and minimum bend radius.
Design Rule Questions
How far should a hole be from the edge of a die-cut part? For holes up to 5/8″ in diameter, Mag-Knight recommends at least one hole diameter of material between the hole and the part edge. Holes larger than 5/8″ need at least 0.30″ of material.
How close can two cut lines or holes be in a steel rule die? Parallel cut lines, including the web between two holes, should be at least one material thickness apart. Closer rule can crush, tear or distort the material, and slugs can pack into the die.
What is the minimum bend radius for a steel rule die? About 1/16″ for softer materials cut with thin rule and 3/32″ for harder materials that need thicker rule.
What is the smallest hole Mag-Knight can die cut? Holes and cutouts under 0.25″ can be cut but are priced as complex parts. Holes under 0.125″ also slow the press.
Engineering Guides
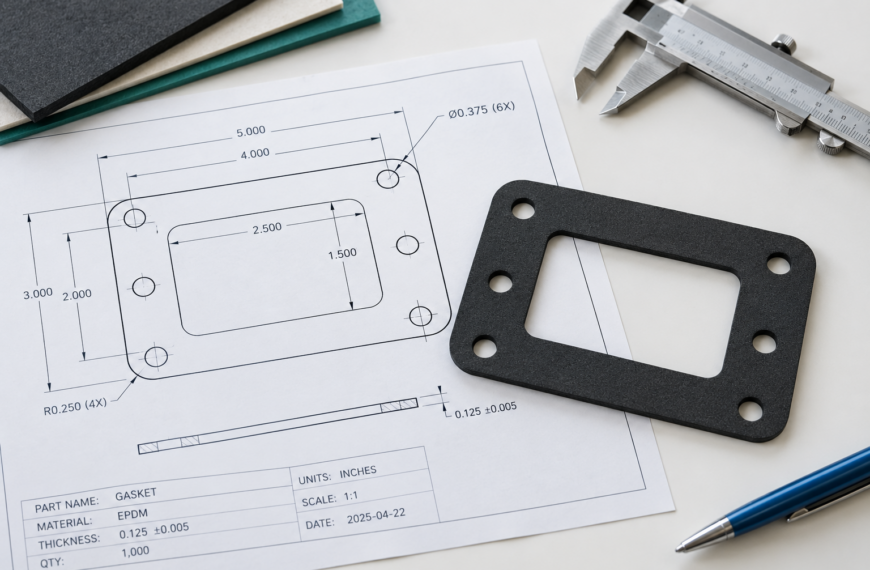
What Information Do I Need to Get a Die-Cutting Quote?
Skip the back and forth and use our new instant…
Laser Cutting vs. Die Cutting: Which Is Right for Your Part?
The short answer: die cutting wins on cost per part…
Choosing a Die-Cut Material by Application: A Buyer’s Guide
Most people researching die-cut materials don’t start with “what is…
What Materials Can Be Die Cut? A Complete Guide
When engineers, designers, and purchasing teams need a custom gasket,…