

Skip the wait and get an instant die price from your PDF or DXF by using our new Instant Online Estimator.
A steel rule die about the size of a piece of paper, with a few simple cut lines or holes, typically runs around $200. Price goes up from there as the part gets bigger, the shape gets more complex, or the material gets harder to cut. Below is what actually drives that number, using how Mag-Knight prices dies day to day.
The Baseline: What a Simple Die Costs
For a paper-sized die with a handful of straight or gently curved cut lines, $200 is a realistic starting point. That price covers the steel rule itself, bending it to your shape, and mounting it into a base ready to run on press. From there, three things move the price: size, feature count, and material hardness. Our custom die cutting page has more on how we scope a new die once we see your drawing.
What Drives the Price Up
Size and feature count are the most intuitive factors: a bigger die needs more steel and more bending, and more cut lines, perforations, or crease lines mean more setup work before the die ever touches a press.
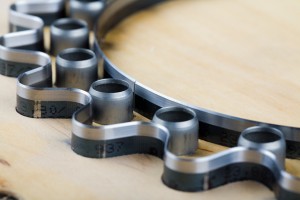
Material hardness is the less obvious one, and it matters more than most people expect. Softer materials like foam and soft rubber cut cleanly with a thin rule, but harder materials such as hard plastics and harder-durometer rubbers need a thicker rule to hold up under repeated impact. Thicker rule costs more outright, and it also cannot bend into fine detail as easily as thin rule can, which limits how intricate a shape can be for a given material.
| Material Type | Typical Rule Thickness | Minimum Bend Radius | Fine Detail Capability |
|---|---|---|---|
| Soft foam, soft rubber | Thin rule | 1/16″ | High, tight curves and fine features are practical |
| Hard plastics, harder rubbers | Thick rule | 3/32″ | Lower, sharp inside corners and tiny features get harder to hold |
If your part has fine internal detail and needs to be cut from a harder material, that combination is usually where die cost climbs the most, since it can mean designing around a larger minimum bend radius rather than just paying more for steel.
Why Rule Thickness Matters for Your Design
The practical takeaway for engineers: if your material is on the harder end, design features with a bend radius at or above 3/32″ wherever possible. Trying to force a tight radius into thick rule usually means either a redesign later or a die that doesn’t hold up as well in production. If you’re not sure where your material falls, our engineering library has additional reference material on rule selection and design-for-manufacturability, and it’s worth a look before finalizing a drawing.
You Own the Die You Pay For
When Mag-Knight builds your die, you own it. You’re paying for the tooling, so the tooling is yours, the same way it would be if you commissioned any other custom tool. What’s different is that we store it in-house at no extra charge, so it’s ready to run again the moment you place a reorder rather than needing to be rebuilt or shipped back and forth. That’s part of why getting a die scoped correctly the first time matters. It’s not a one-time expense, it’s an asset that sits on our shelf working for you on every future order.
How Long Does a Die Last?
A properly maintained die can produce tens of thousands of impressions before it needs rework, though the exact number depends heavily on the material being cut and how the die is run. Harder materials wear a die faster than soft ones, which is another reason the rule-thickness decision at the start matters for total cost over the life of the tooling, not just the upfront price. Proper storage and handling between runs, which we manage as part of keeping your die in-house, also extends usable life meaningfully compared to a die that gets shipped and reinstalled every order.
Want to Go Deeper on Die Design?
If you want to understand die design beyond pricing, Mag-Knight has a full video series on die design available in the sidebar of our website, covering rule selection, bend radius, and layout considerations in more depth than a single blog post can. It’s a good next step if you’re designing a part in-house before sending us a drawing.
Getting an Accurate Die Quote
Because size, feature count, and material all affect price, the fastest way to get a real number instead of an estimate is to send your drawing and material spec through our quotation page. If you’re still finalizing the design, our rapid prototyping option lets you validate the part with laser cutting first, so you’re not paying for a die until the design is locked. For a broader look at how tooling and production cost combine into a per-part price, see our full cost breakdown.
Frequently Asked Questions
How much does a basic custom die cost? A steel rule die about the size of a piece of paper with a few simple features typically costs around $200. Larger or more complex dies cost more.
Why do harder materials cost more to tool for? Harder materials like hard plastics and higher-durometer rubbers require thicker steel rule to hold up under repeated cutting. Thicker rule costs more and cannot be bent into as fine a detail as thinner rule used for softer materials.
What is the minimum bend radius for a die? For softer materials cut with thin rule, a bend radius around 1/16″ is typical. For harder materials requiring thicker rule, the minimum bend radius is generally 3/32″.
Who owns the die after it’s made? The customer does. Since you pay for the tooling, it belongs to you. Mag-Knight stores it in-house at no extra charge so it’s ready for future reorders.
How many parts can a single die produce? A well-maintained die can typically produce tens of thousands of impressions, though the exact figure depends on the material being cut and how the die is used and stored between runs.
Does die storage cost extra? No. Mag-Knight stores customer-owned dies in-house as part of the service, so reorders don’t require rebuilding or reshipping tooling.
Where can I learn more about die design before I submit a drawing? Our website’s sidebar hosts a full video series on die design covering rule selection, bend radius, and layout. Our engineering library also has written reference material on the same topics.
Ready to find out what your die will cost? Request a quote with your drawing and material, or reach out through our contact page if you’d like to talk through the design first.

Pingback: How Many Parts Do I Need Before Die Cutting Is Cost Effective?
Pingback: How To Reduce The Cost Of A Die-Cut Part: 10 Practical Ways